Application Technical Brief — gentle drying and oxygen protection for dairy, protein, coffee, flavour and functional powder production
TWO SYSTEMS, ONE CLOSED LOOP
| SPRAY DRYING PLATFORM | NITROGEN PLATFORM |
|---|---|
| Co-current tower — droplets meet the hottest gas first and leave through the coolest zone Seconds-level residence protects proteins, vitamins and volatile aromas Integrated fluid bed for after-drying, cooling and agglomeration Sanitary 316L contact parts, CIP-cleanable, hygienic design | On-site N2 generation (PSA / membrane) — no cylinders, no logistics Closed-loop drying gas holds loop O2 below 2% for fat-rich formulations Inerting of conveying, sieving and silo storage; low dew point to −40…−60 °C Headspace flushing keeps packaged residual O2 below 1–2% |
1 APPLICATION OVERVIEW
Food-grade powders — whole-milk and whey powders, infant-formula bases, plant and animal proteins, instant coffee and tea extracts, flavour systems, egg products and functional ingredients — are made by removing water from liquid concentrates while preserving nutrition, flavour, colour and solubility. Spray drying is the industry-standard route: atomized droplets meet hot gas and dry to particles within seconds.
The same products, however, are typically rich in milk fat, unsaturated oils, proteins and volatile aromas — all highly sensitive to heat and oxygen. Food-safety regulations add a third dimension: hygienic equipment design, clean-in-place capability, controlled-atmosphere handling and protection against combustible-dust hazards. This brief describes how ANVORE spray dryers, combined with ANVORE on-site nitrogen generation solutions, form one closed, low-oxygen production line for premium food-grade powders.
2 THE CHALLENGE: HEAT, OXYGEN AND HYGIENE
| PRESSURE | WHAT IT MEANS FOR THE POWDER LINE |
|---|---|
| Thermal degradation | Proteins denature, vitamins degrade, sugars and acids brown; hygroscopic amorphous powders reach their sticky point and deposit on chamber walls. |
| Fat oxidation | Milk fat and omega-rich oils oxidize during long, oxygen-rich drying and again in the package, producing cardboard off-flavours and shortening shelf life. |
| Microbial & hygiene demands | Dairy and protein feeds require pasteurization upstream and sanitary, CIP-cleanable equipment throughout; wet surfaces must never sit at warm temperatures. |
| Combustible dust | Fine organic powders form explosive atmospheres; hot zones and dust layers must be managed, and inert gas is the most robust safeguard. |
3 TWO SYSTEMS, ONE CLOSED LOOP
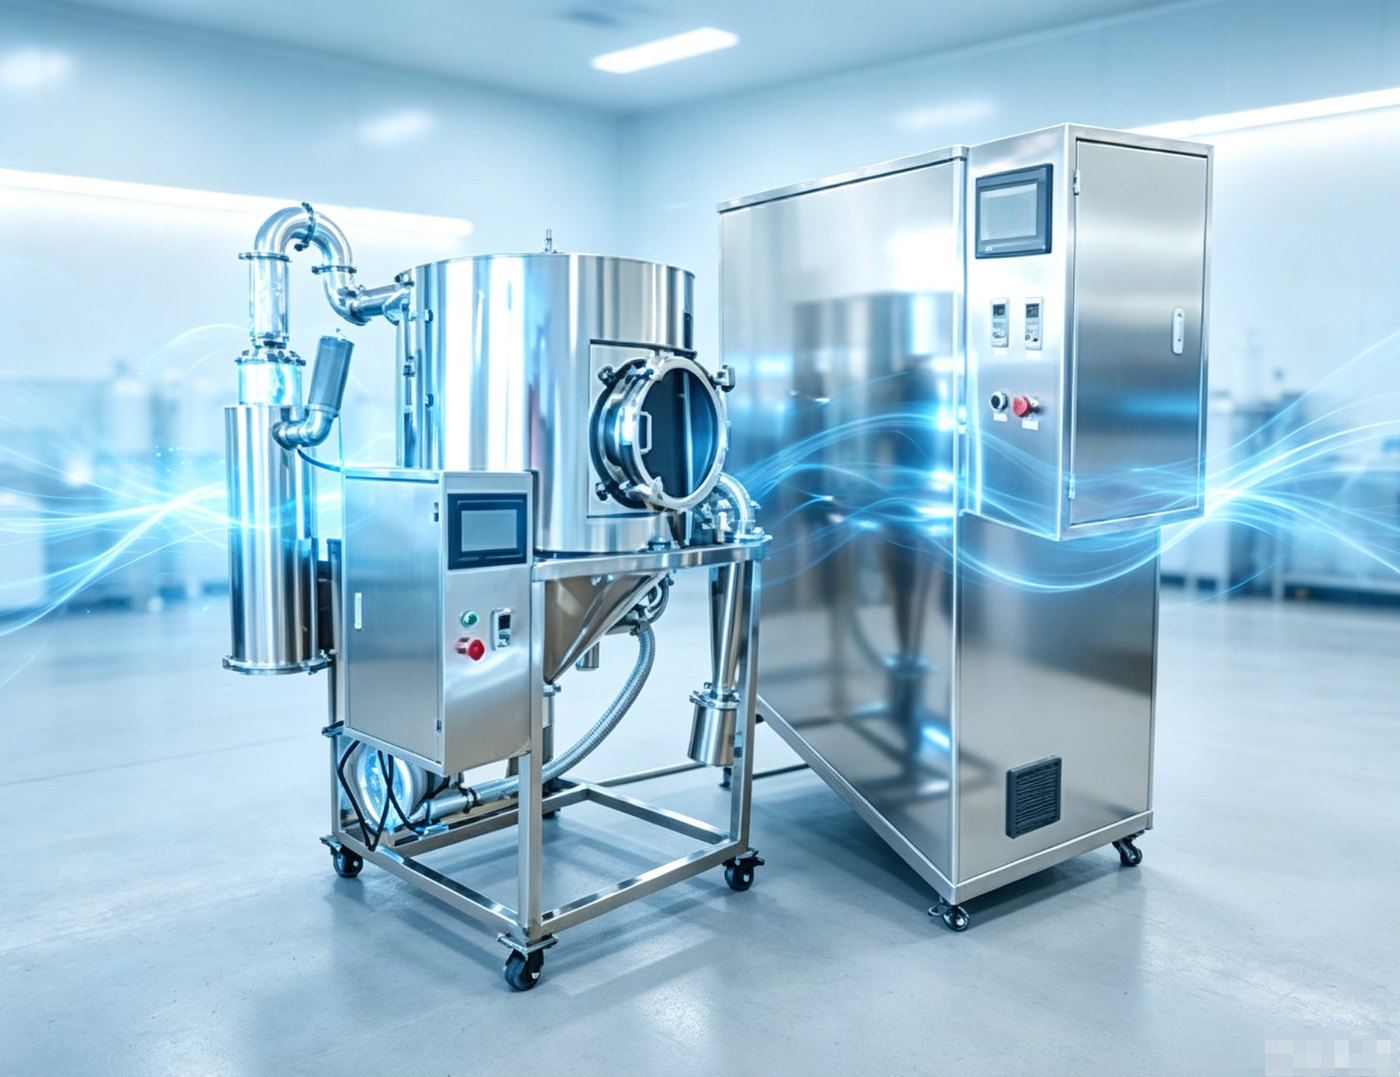
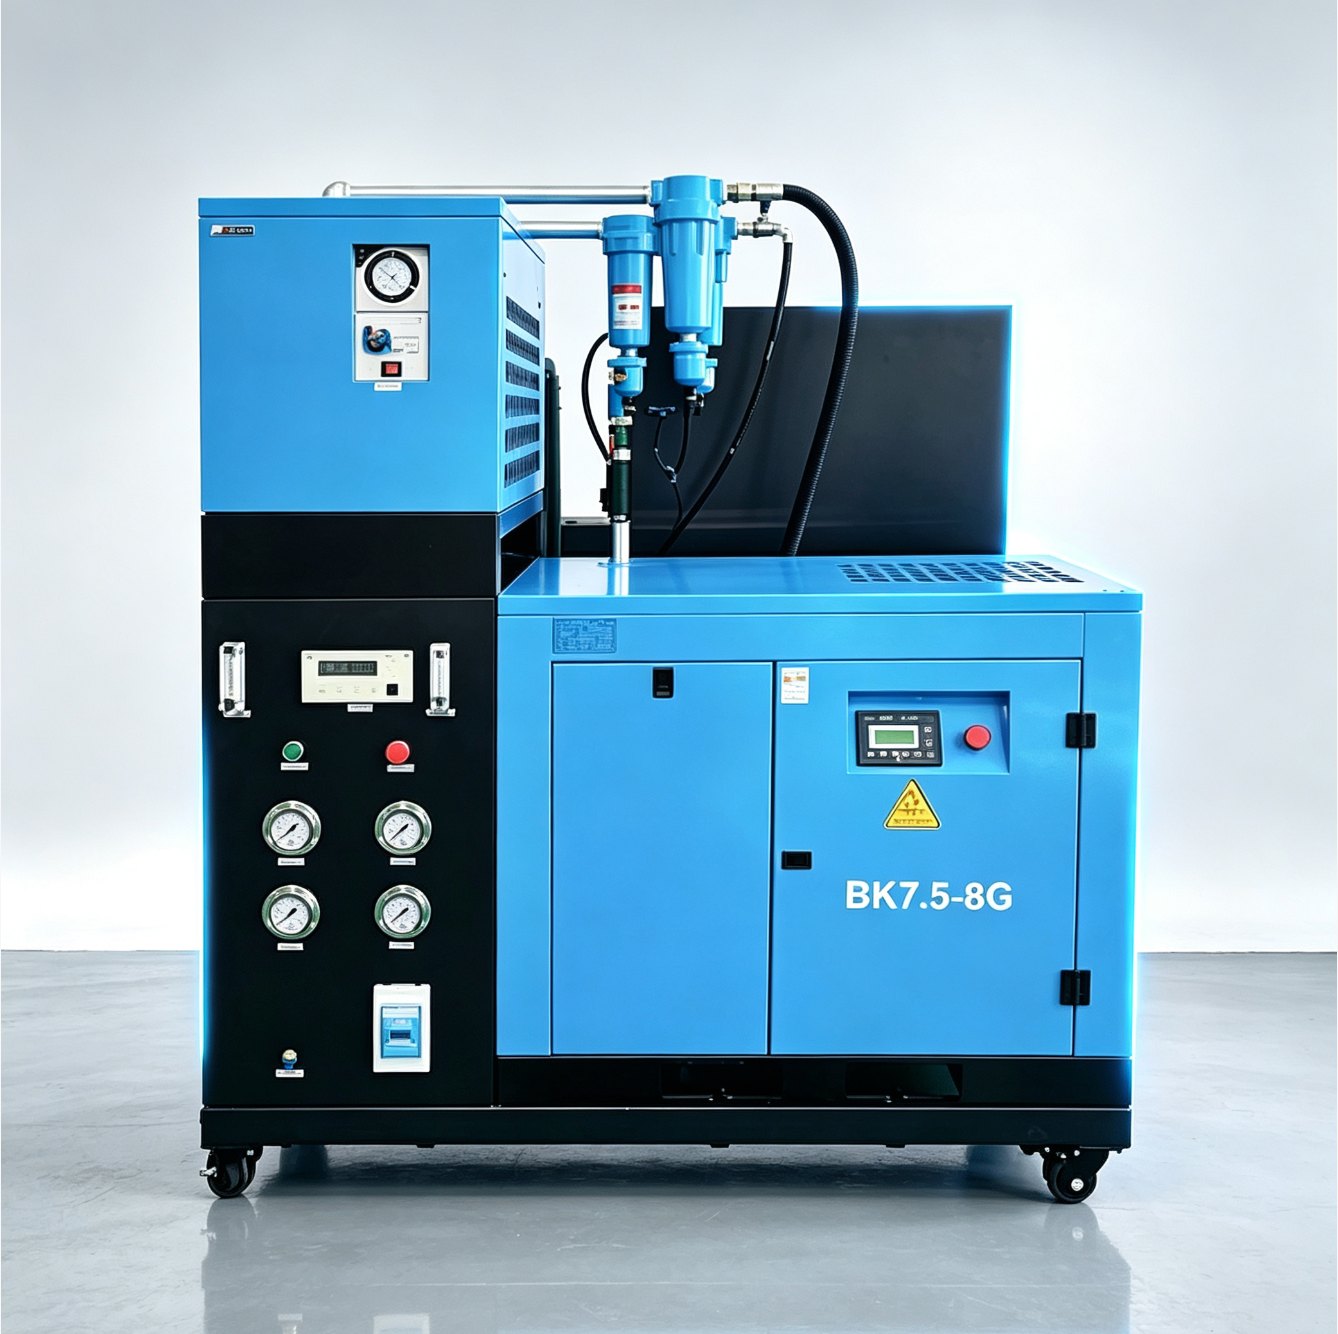
ANVORE engineers the drying tower and the nitrogen plant as a single system. Where the formulation is fat-rich or oxygen-sensitive, the dryer runs on recirculated nitrogen instead of air: the loop is continuously monitored, oxygen is held below 2%, and fine powder is moved, stored and packed under inert gas. Where the formulation is robust, the same nitrogen plant still protects conveying, silos and packaging while the dryer runs on dehumidified air.
WHERE NITROGEN TOUCHES THE LINE
| LINE STAGE | NITROGEN ROLE | TYPICAL TARGET |
|---|---|---|
| Spray drying gas | Inert recirculated drying medium with online O2 control | Loop O2 < 2% |
| Powder conveying | Dense-phase pneumatic conveying on nitrogen | Dust-free, inert transfer |
| Silo & intermediate storage | Continuous or demand blanketing of headspace | O2 < 2% at headspace |
| Packing & sealing | Headspace flushing and sealing under N2 | Residual O2 < 1–2% |
4 PROCESS FLOW
The powder line and the nitrogen loop operate in parallel. Solid arrows follow the product; dashed arrows mark the three points where nitrogen enters the line.
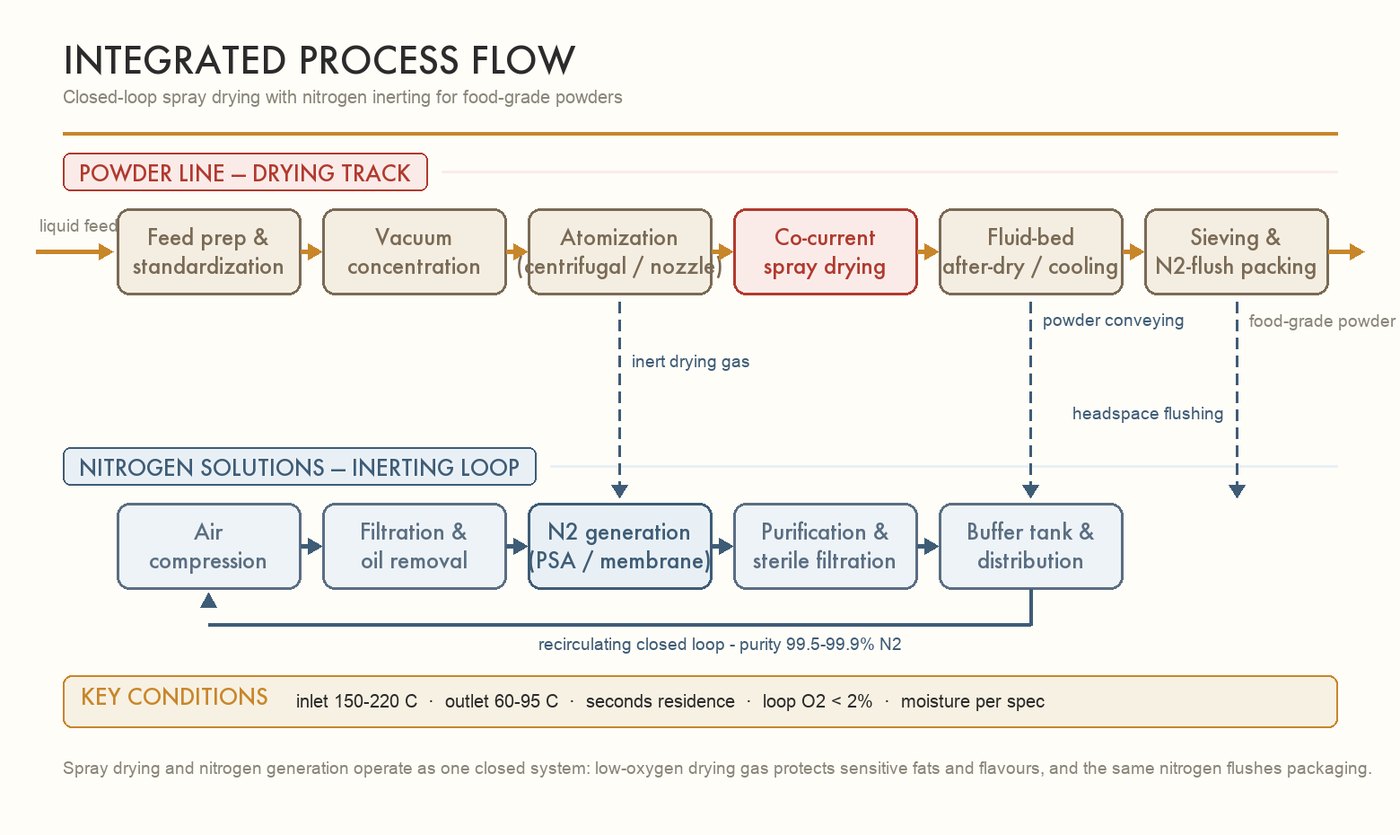
4.1. Feed preparation & standardization —Mixing, dissolution, HTST pasteurization where required, and fine filtration to protect the atomizer.
4.2. Vacuum concentration —Gentle falling-film evaporation raises solids to 40–55%, cutting dryer load and specific energy per kilogram of powder.
4.3. Atomization —Centrifugal disc or high-pressure nozzle produces uniform droplets matched to the target particle size.
4.4. Co-current spray drying —Droplets meet hot filtered air — or recirculated nitrogen below 2% O2 for sensitive formulas — and dry within seconds at controlled outlet temperature.
4.5. Fluid-bed after-drying & cooling —Final moisture trim, cooling and optional agglomeration for instant products.
4.6. Sieving & nitrogen-flushed packing —In-line sieving, blending, and packing under a nitrogen sweep; headspace residual O2 is verified before sealing.
5 TYPICAL PARAMETERS & QUALITY OUTCOMES
| PARAMETER | TYPICAL RANGE |
|---|---|
| Feed solids (after concentration) | 40–55% TS, application-dependent |
| Drying gas inlet | 150–220 °C (air) / 150–180 °C (nitrogen loop) |
| Drying gas outlet | 60–95 °C, product-controlled |
| Drying loop oxygen | < 2% O2, online monitoring with automatic purge |
| Nitrogen purity / dew point | 99.5–99.9% N2 / −40…−60 °C after drying |
| Packaged residual oxygen | < 1–2% in headspace, verified per batch |
QUALITY OUTCOMES
Powder quality —lower surface free fat and improved wettability, dispersibility and flowability of the finished powder
Shelf life —reduced oxidation during drying and storage translates directly into longer shelf life and cleaner flavour
Microbial control —HTST upstream plus a closed, CIP-cleanable, hygienic line supports consistent food-safety performance
Process safety —inerting of drying, conveying and packing removes the oxygen a dust explosion needs
FOOD-GRADE BY DESIGNSanitary 316L product-contact parts · CIP-cleanable · food-contact-compliant materials · hygienic welded pipework · online O2 and dew-point monitoring · full validation support
6 CONCLUSION
For food-grade powders, product quality is decided in the seconds between droplet and particle — and preserved in the months between packing and consumption. ANVORE integrates spray drying and on-site nitrogen generation into one closed, low-oxygen line: gentle thermal profiles protect nutrition and aroma, inert handling protects fats from oxidation and the plant from dust hazards, and nitrogen-flushed packing locks shelf life into every bag and can.
Configurations scale seamlessly from laboratory and pilot dryers for recipe development to multi-storey production towers with integrated nitrogen plants. ANVORE provides process trials with your product, sizing and layout engineering, commissioning, operator training and long-term service support.