Stainless Steel Multi-Function Reactor
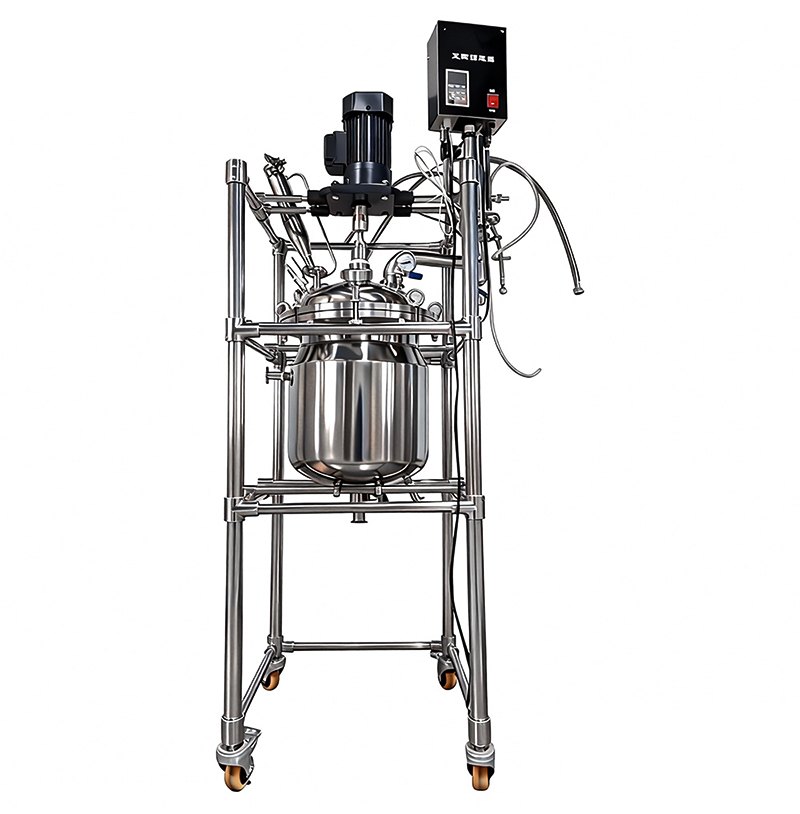
The AV-50R is a 50-litre floor-standing reactor built around a SUS316L inner vessel, a vacuum-tight SUS304 jacket shell, a heavy-duty top-drive.
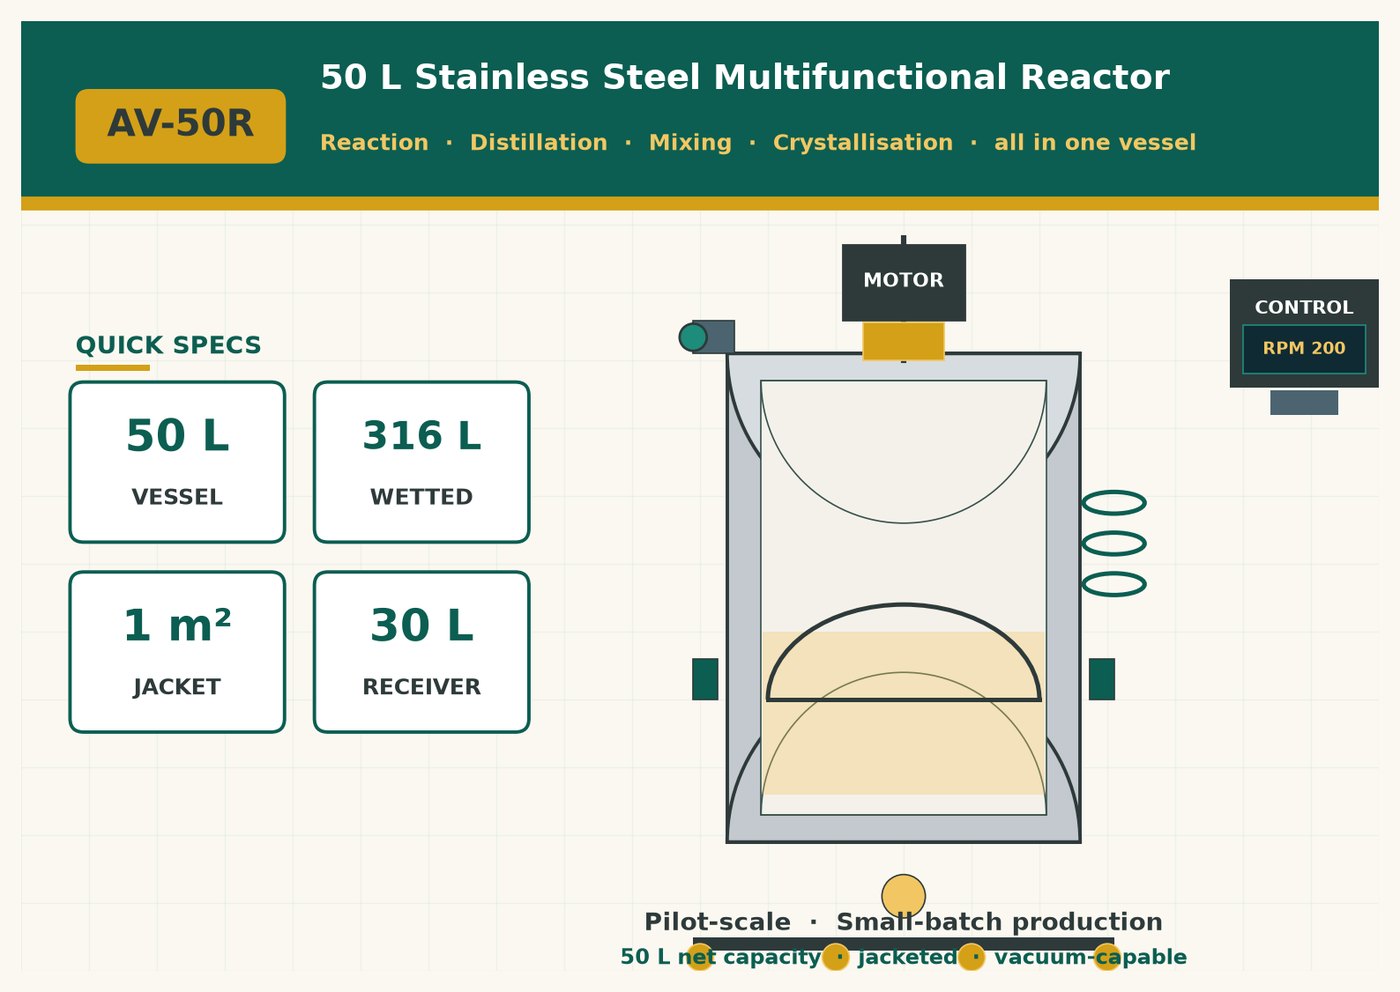
| AV-50R · 50 L STAINLESS STEEL MULTIFUNCTIONAL REACTOR Reaction · Distillation · Mixing · Crystallisation One jacketed vessel replaces four separate pieces of equipment. Use it for batch reactions, atmospheric or vacuum distillation, slurry mixing and controlled crystallisation — ideal for pilot plants, contract labs and small-batch API or botanical production. |
| 50 L VESSEL | 316 L WETTED | 1 m² JACKET | 30 L RECEIVER |
WHY AV-50R
DESIGN & STRUCTURE
- The AV-50R is a 50-litre floor-standing reactor built around a SUS316L inner vessel, a vacuum-tight SUS304 jacket shell, a heavy-duty top-drive motor, an interchangeable agitator (anchor / paddle / propeller), and a multi-coil reflux condenser. Every port, valve and instrument is designed for repeatable batch operation under vacuum and elevated temperature.
- Cutaway of the AV-50 — R · jacketed vessel with reflux condenser (numbered parts are explained below).
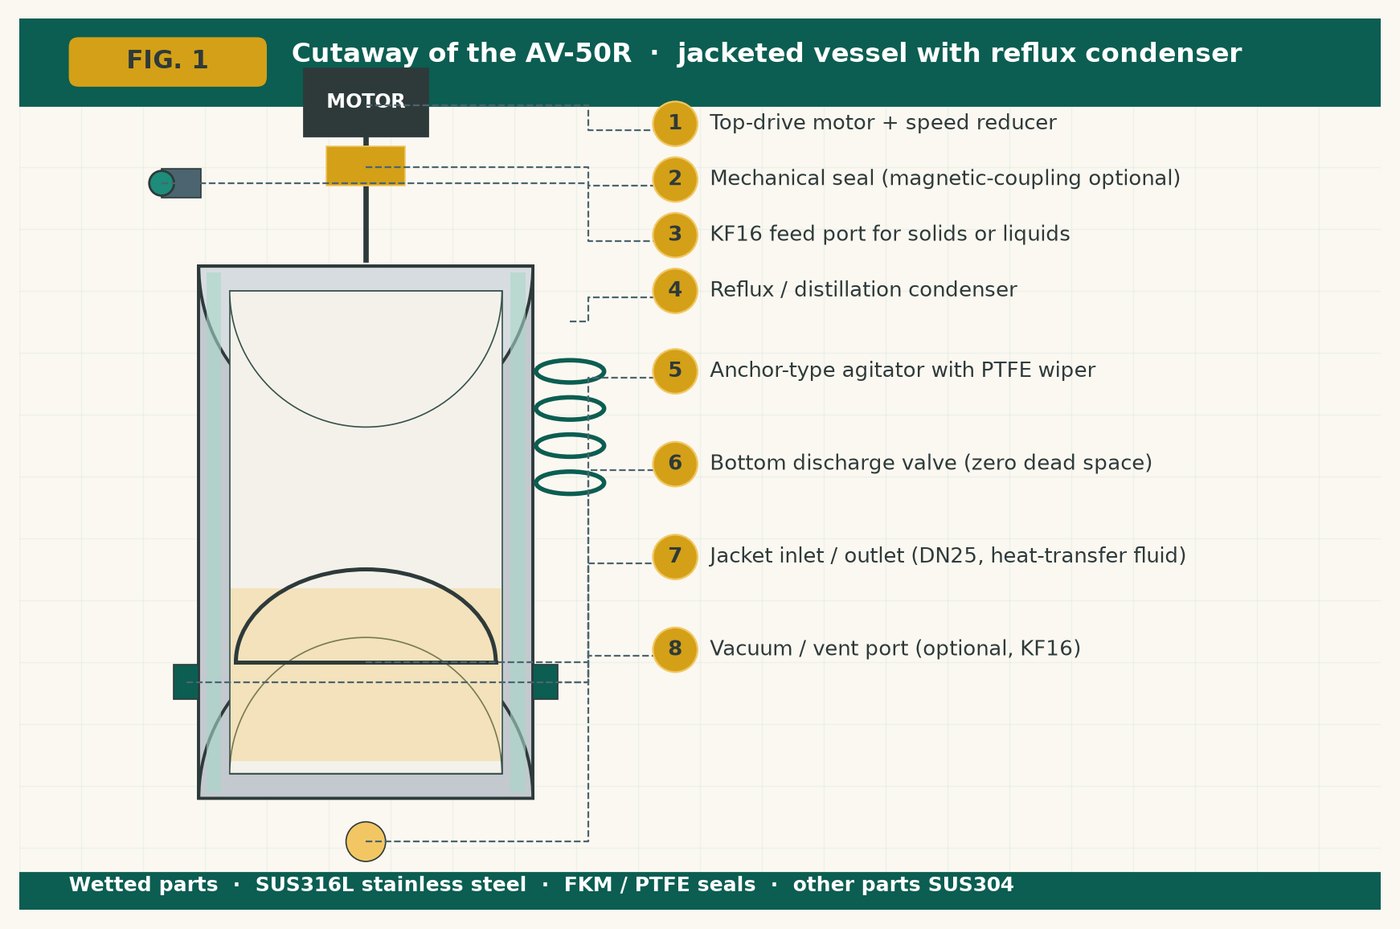
| No. | Component | Role |
|---|---|---|
| 1 | Top-drive motor | 0.75 kW variable-speed drive |
| 2 | Mechanical seal | Magnetic-coupling seal optional for air-free chemistry |
| 3 | KF16 feed port | Solid or liquid charging without opening the lid |
| 4 | Reflux condenser | Multi-coil, diverts vapours to the 30 L receiver |
| 5 | Anchor-type agitator | PTFE wiper blades for viscous and high-solid pastes |
| 6 | Bottom discharge | Zero-dead-space drain valve for crystals and slurry |
| 7 | Jacket inlet / outlet | DN25 ports, accepts heat-transfer fluid |
| 8 | Vacuum / vent port | KF16 connection to the vacuum pump and vent line |
WORKING PRINCIPLE
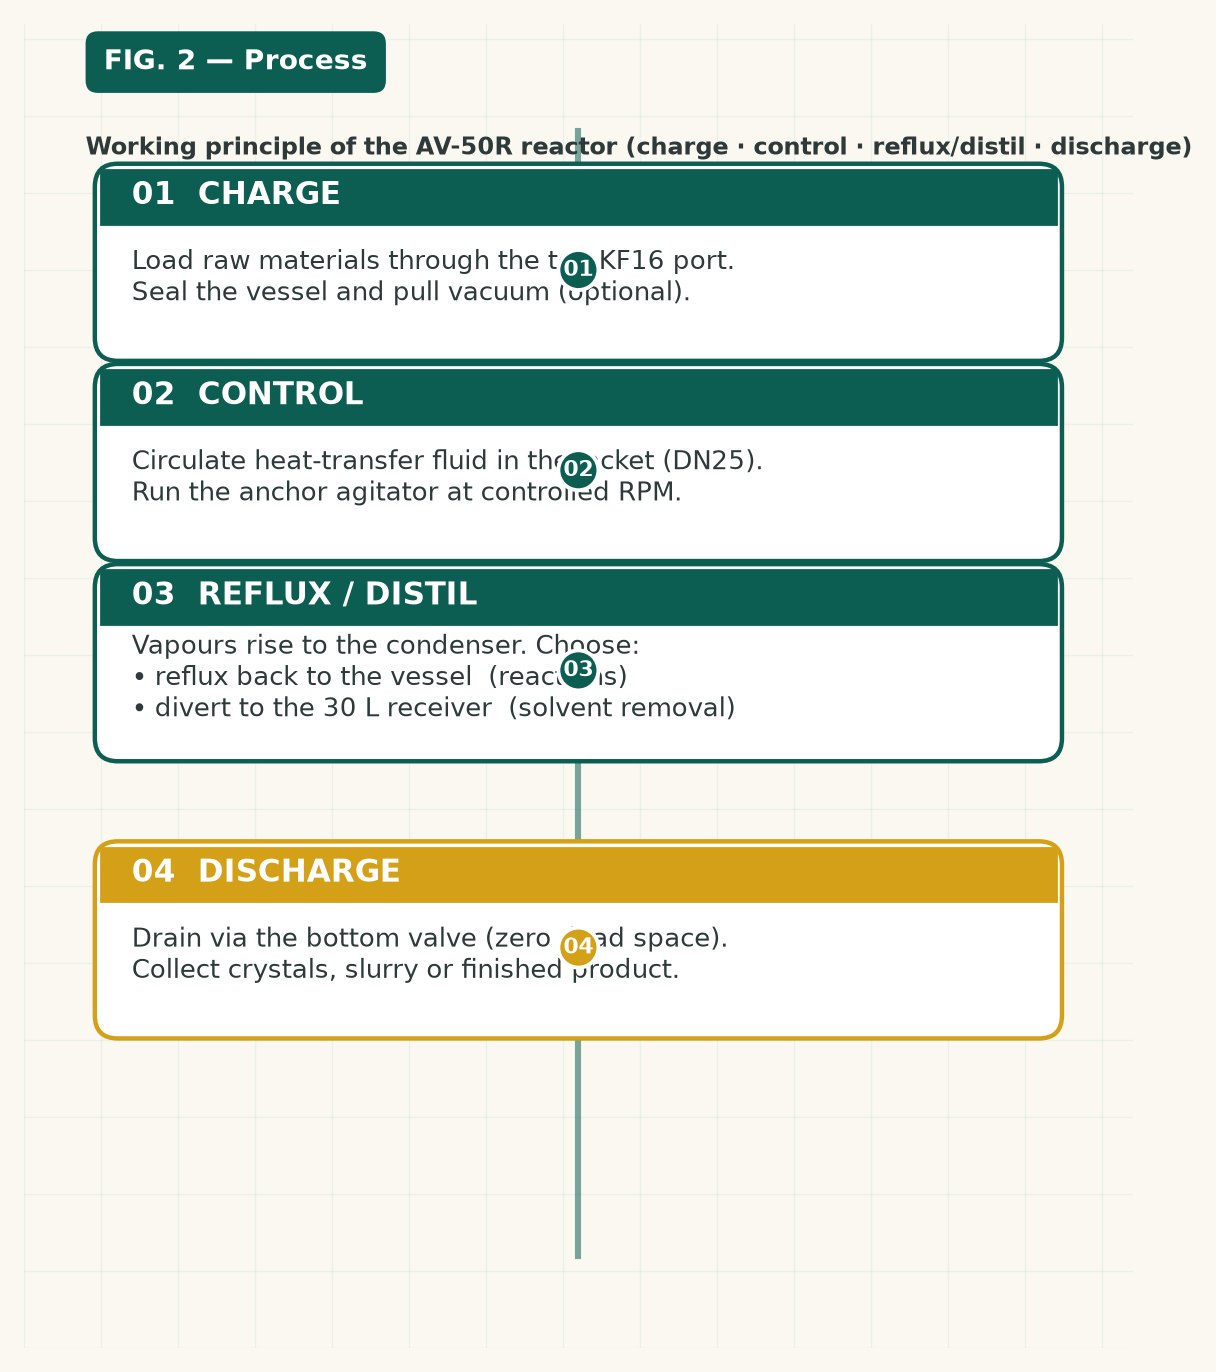
- Fig. 2 — Working principle of the AV-50 — R · charge → control → reflux/distil → discharge.
- 01 · Charge — Load raw materials through the KF16 top port, then seal and pull vacuum (optional) before heating.
- 02 · Control — Circulate heat-transfer fluid through the 1 m² jacket and run the anchor agitator at the target RPM — the same vessel handles exothermic and endothermic steps.
- 03 · Reflux or distil — Vapours rise to the condenser. Choose full reflux (to keep the reaction at temperature) or divert to the 30 L receiver (to strip solvent or collect a fraction).
- 04 · Discharge — Open the bottom valve to drain the slurry. The zero-dead-space design leaves no residue — ideal for crystals, suspension products and small-batch AP Is.
- Net result: one vessel replaces a separate reactor + still + mixer + crystalliser, with fewer product transfers, fewer cleaning cycles and a much smaller footprint.
TECHNICAL SPECIFICATIONS
- * Specifications follow the manufacturer’s published data sheet for model AV-50R.
| Parameter | Value |
|---|---|
| Model | AV-50R |
| Type | Stainless steel multifunctional reactor (batch) |
| Working volume | 50 L |
| Wetted material | SUS316L stainless steel |
| Other material | SUS304 stainless steel shell |
| Jacket heating / cooling area | 1 m² |
| Receiver volume | 30 L |
| Sealing material | PTFE (polytetrafluoroethylene) |
| Agitator type | Anchor / paddle / propeller (interchangeable) |
| Motor power | 0.75 kW |
| Power supply | 220 V 50/60 Hz, or 380 V 50/60 Hz (other voltages on request) |
| Jacket connection | DN25 inlet / outlet |
| Seal option | Mechanical seal (standard) or magnetic-coupling seal |
| Discharge | Bottom drain valve, zero dead space |
| Coolant connection | DN15 inlet / outlet |
| Overall dimensions (L×W×H) | 195 × 100 × 220 cm |
| Standard accessories | Condenser, 30 L receiver, anchor agitator, motor, controller |
APPLICATIONS
- The AV-50R is widely used wherever a 50-litre batch has to be reacted, distilled, mixed or crystallised in a single sealed vessel — typical industries and duties include:
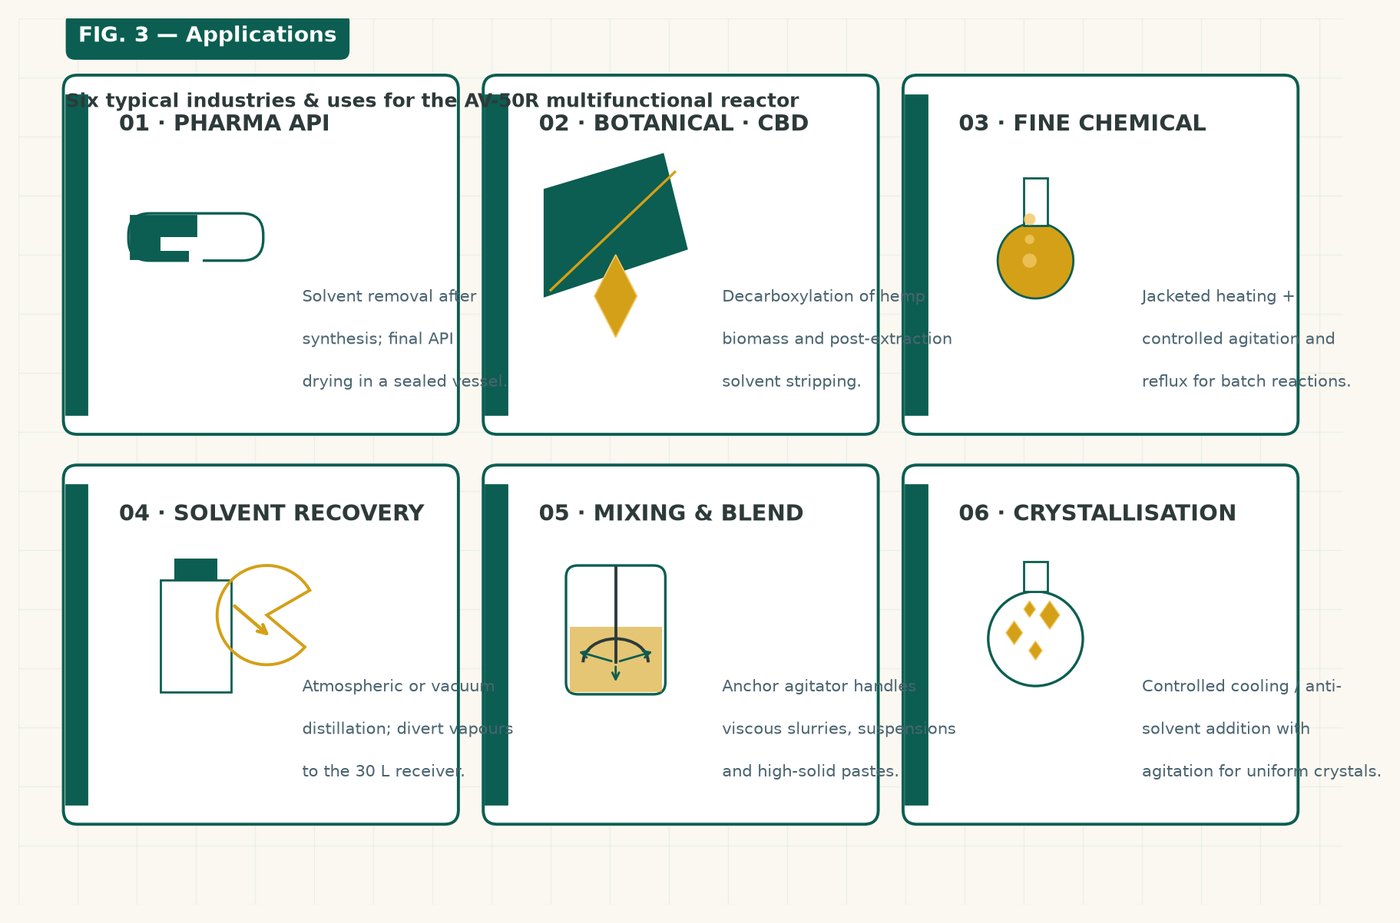
- Fig. 3 — Six typical industries and uses for the AV-50R multifunctional reactor: pharma AP Is, botanical / CBD extracts, fine chemicals, solvent recovery, mixing and crystallisation.
| Industry | Typical duties |
|---|---|
| Pharma & API | Solvent removal after synthesis and final API drying in a sealed, vacuum-capable vessel. |
| Botanical & CBD extracts | Decarboxylation of hemp biomass and post-extraction solvent stripping. |
| Fine & specialty chemicals | Jacketed heating with controlled agitation and reflux for batch reactions. |
| Solvent recovery | Atmospheric or vacuum distillation; divert vapours to the 30 L receiver. |
| Mixing & blending | Anchor agitator handles viscous slurries, suspensions and high-solid pastes. |
| Crystallisation | Controlled cooling or anti-solvent addition with agitation for uniform crystals. |
SERVICE & CONTACT
- We back the AV-50R with full pre-sales and after-sales support from the factory:
- • One-stop complete systems — we can supply matching vacuum pump, heating/cooling circulator, low-temperature chiller and PTFE transfer lines so the reactor ships ready to run.
- • Customisation — vessel volume, agitator type, motor, control panel and seal configuration can be tailored to the process.
- • Commissioning — installation guidance, on-site commissioning and operator training are available on request.
- • Warranty & spares — 12-month warranty plus long-term spare-parts supply and remote diagnostic support.
More Reactors Overview
AV20RLab Stainless Steel Reactor
The AV-20R is a 20-litre floor-standing reactor built around a SUS316L inner vessel, a vacuum-tight SUS304 jacket shell, a heavy-duty top-drive.
View Product →AV100RStainless Steel Reactor
Console view of the AV-100R — the left panel summarises the headline specs; the right side shows the jacketed vessel, reflux condenser and 1.5 kW top.
View Product →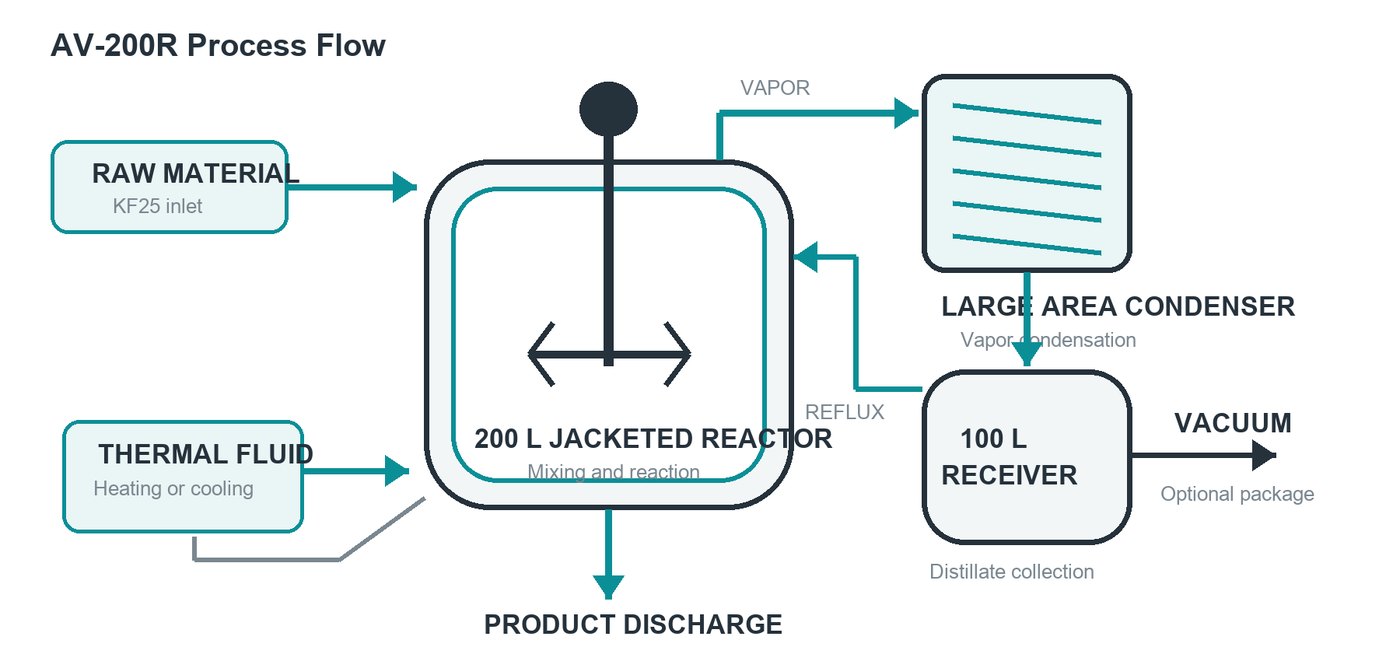 AV200R
Chemical Stainless Steel Multifunctional Reactor Vessel
AV-200R is designed for pilot plants and small-batch production that require controlled reaction and efficient separation in a compact footprint.
View Product →Reactors Overview
A jacketed reactor controls a reaction by controlling the temperature of the fluid circulating through the jacket that surrounds the vessel. Because heat is added or removed throug
Learn More →