Stainless Steel Reactor
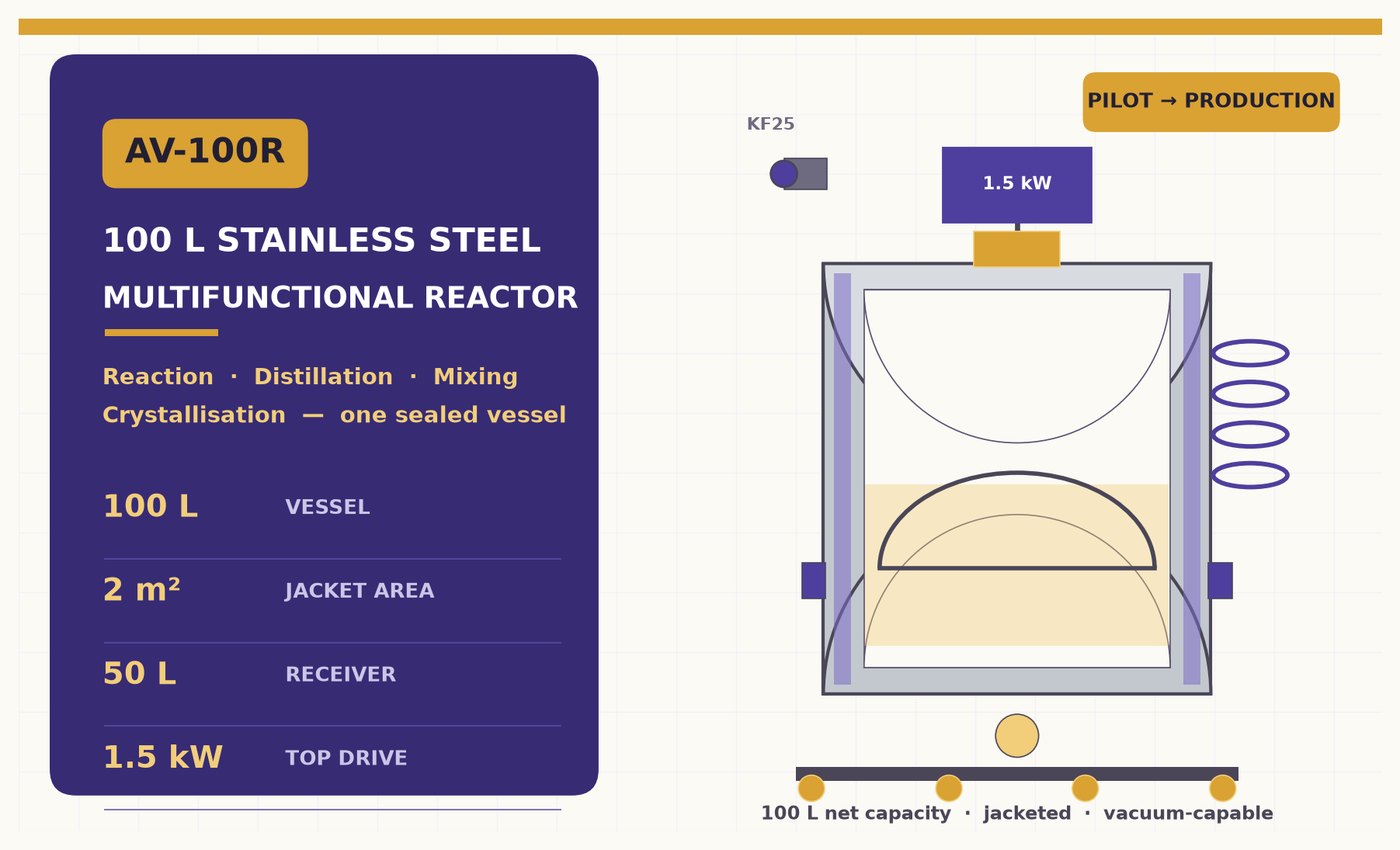
Console view of the AV-100R — the left panel summarises the headline specs; the right side shows the jacketed vessel, reflux condenser and 1.5 kW top.
Console view of the AV-100R — the left panel summarises the headline specs; the right side shows the jacketed vessel, reflux condenser and 1.5 kW top drive.
Why AV-100R
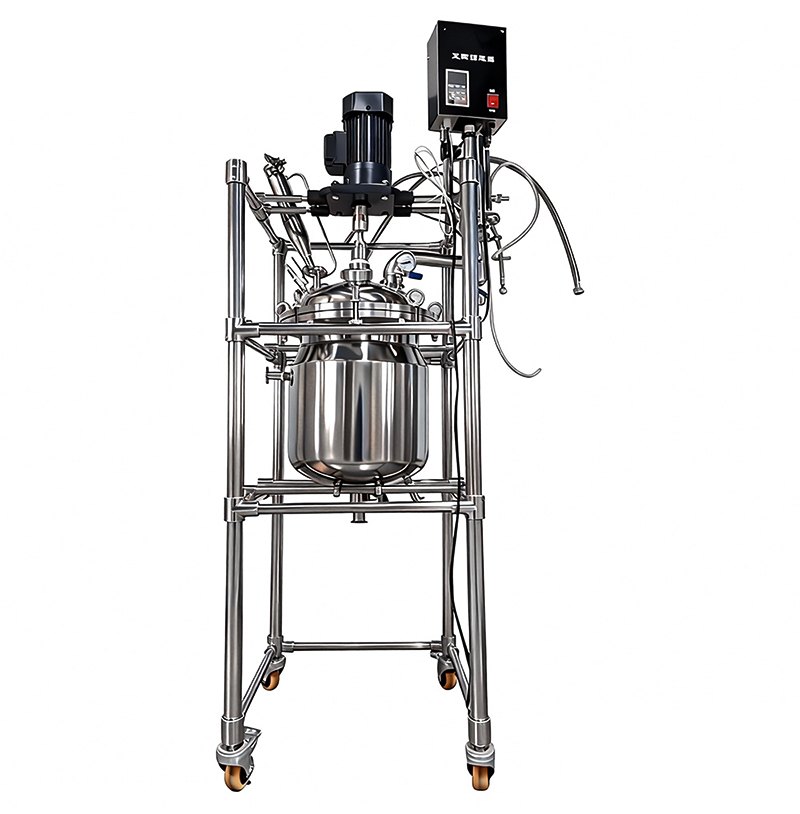
The AV-100R moves you from bench-top evaporation to pilot and small-batch production — without moving to a fixed industrial skid. It gives a 100 L net capacity in a single, fully sealed vessel that can react, reflux, distil, mix and crystallise. Built on SUS316L wetted parts and SUS304 outer shell, it handles service across pharmaceutical, botanical, fine-chemical and solvent-recovery workflows.
| 100 L VESSEL | 2 m² JACKET | 50 L RECEIVER | 1.5 kW TOP DRIVE |
Design & Structure
| 01 | Top-drive motor — 1.5 kW variable speed, anchor / paddle / propeller interchangeable |
|---|---|
| 02 | Mechanical seal — PTFE-faced, magnetic-coupling upgrade available |
| 03 | KF25 feed port — larger than the bench-top line — handles solids and viscous slurries |
| 04 | Reflux condenser — large heat-exchange area, fast cool-down |
| 05 | Anchor agitator — PTFE wiper blades, three interchangeable geometries |
| 06 | Bottom discharge — zero-dead-space valve drains slurry, crystals or finished product |
| 07 | Jacket inlet / outlet — DN25 connections |
Working Principle
- One sealed vessel — four stages from charge to discharge. Vapour can be fully refluxed (reaction) or diverted to the receiver (distillation).
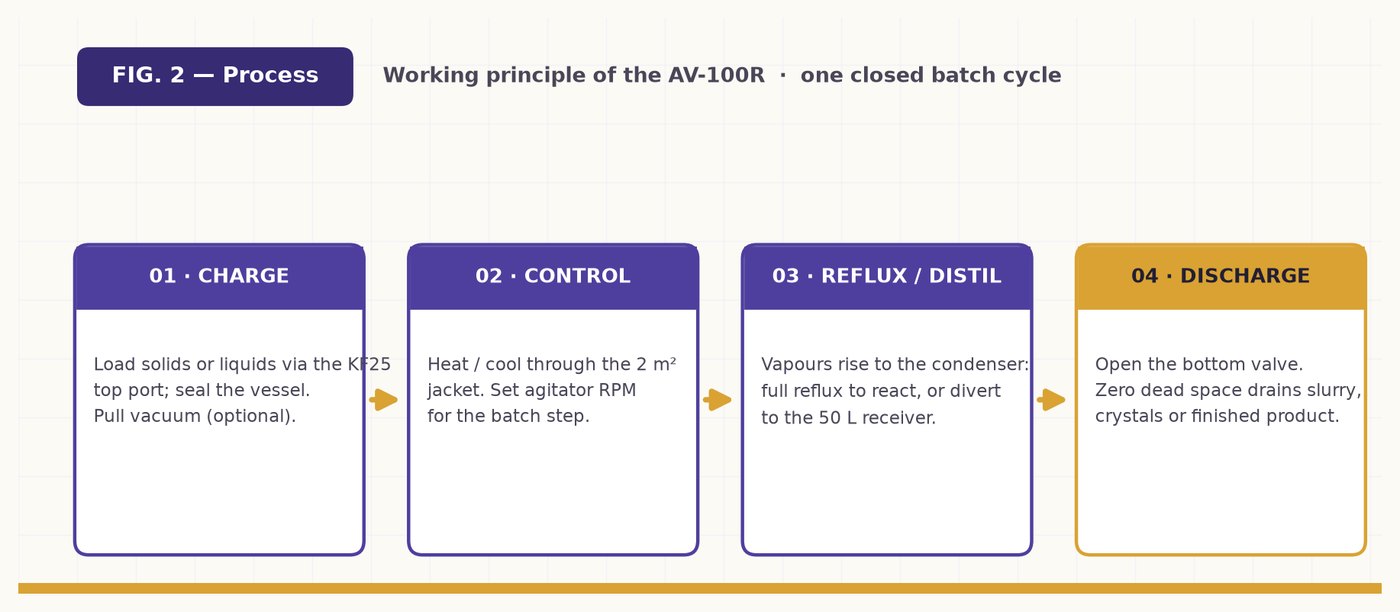
| 01 Charge: Load raw materials via the KF25 port. | 02 Control: Heat or cool through the 2 m² jacket. Set RPM for the reaction. | 03 Reflux: Reflux to react longer, or divert condensate to the 50 L receiver. | 04 Discharge: Open bottom valve — zero dead space, full product recovery. |
| 05 — Technical Specifications | |
|---|---|
| Parameter | Specification |
| Model | AV-100R |
| Vessel net volume | 100 L |
| Collection receiver | 50 L |
| Wetted material | SUS316L stainless steel |
| Outer shell material | SUS304 stainless steel |
| Jacket heat-exchange area | 2 m² |
| Agitator power | 1.5 kW |
| Agitator geometry | Anchor / paddle / propeller (interchangeable) |
| Seal | Mechanical seal (PTFE) — magnetic-coupling optional |
| Feed port | KF25 |
| Jacket connections | DN25 inlet / outlet |
| Coolant connection | DN15 |
| Power supply | 220 V / 380 V — 50 / 60 Hz or customized |
| Footprint (L × W × H) | 199 cm × 98 cm × 237 cm |
Applications
- Across six core applications the AV-100R replaces several single-purpose vessels with one sealed, vacuum-capable unit.
| Pharmaceutical API pilot Reaction, crystallisation and solvent swap for small-molecule AP Is under cGMP-style conditions. | Botanical & CBD extraction Ethanol- or water-based extraction and concentration of plant biomass; reflux with mild vacuum. |
|---|---|
| Fine & specialty chemicals Multi-step synthesis, hydrogenation upstream and distillation downstream in one vessel. | Solvent recovery Vacuum distillation of DMF, toluene, methanol or acetone; recover and reuse solvents. |
| Mixing & formulation High-viscosity blending of creams, slurries and intermediates with anchor or paddle impeller. | Crystallisation & drying prep Controlled cooling crystallisation; jacket-fed chiller preps crystals for filtration or tray drying. |
Service
- Customisation — . Volume, agitator geometry, seal type and PLC package can be tailored to your recipe and target throughput.
- Warranty & support. 12-month limited warranty, lifetime remote technical support, on-site commissioning available.
- Lead time. Standard configuration ships in 15 working days; custom builds typically 25–30 working days.
More Reactors Overview
AV20RLab Stainless Steel Reactor
The AV-20R is a 20-litre floor-standing reactor built around a SUS316L inner vessel, a vacuum-tight SUS304 jacket shell, a heavy-duty top-drive.
View Product →AV50RStainless Steel Multi-Function Reactor
The AV-50R is a 50-litre floor-standing reactor built around a SUS316L inner vessel, a vacuum-tight SUS304 jacket shell, a heavy-duty top-drive.
View Product →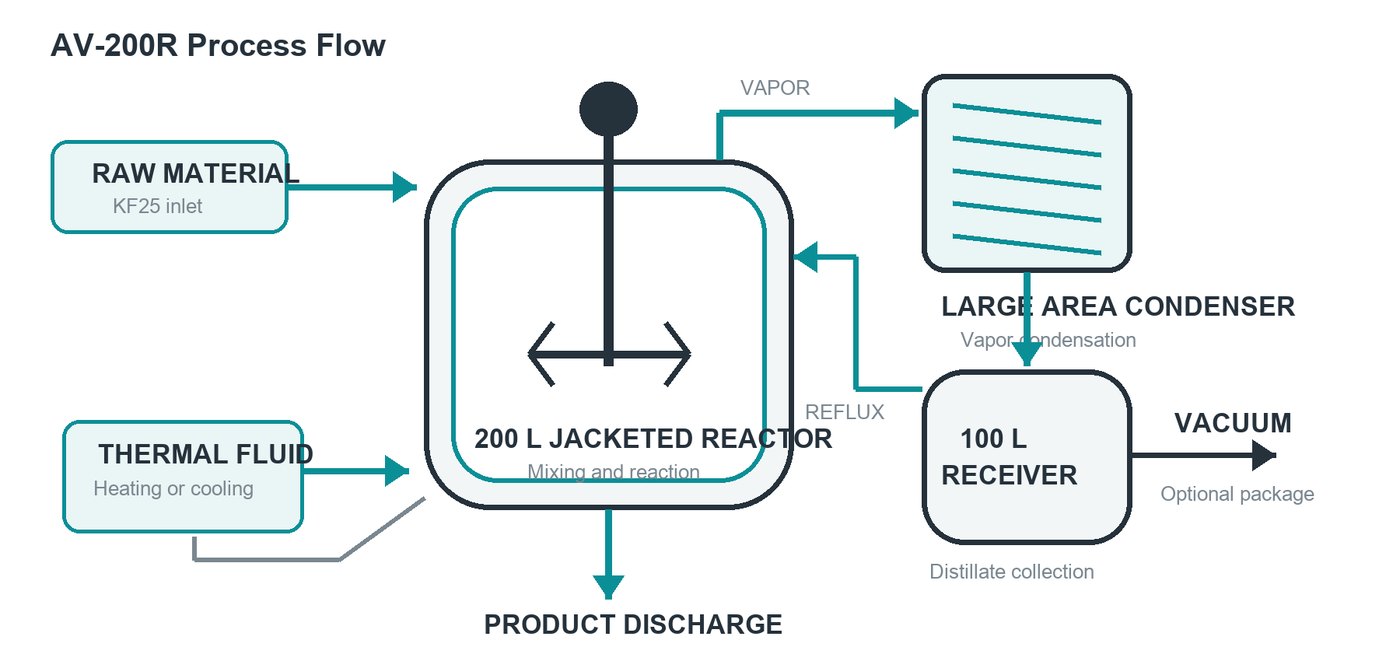 AV200R
Chemical Stainless Steel Multifunctional Reactor Vessel
AV-200R is designed for pilot plants and small-batch production that require controlled reaction and efficient separation in a compact footprint.
View Product →Reactors Overview
A jacketed reactor controls a reaction by controlling the temperature of the fluid circulating through the jacket that surrounds the vessel. Because heat is added or removed throug
Learn More →