Chemical Stainless Steel Multifunctional Reactor Vessel
AV-200R is designed for pilot plants and small-batch production that require controlled reaction and efficient separation in a compact footprint.
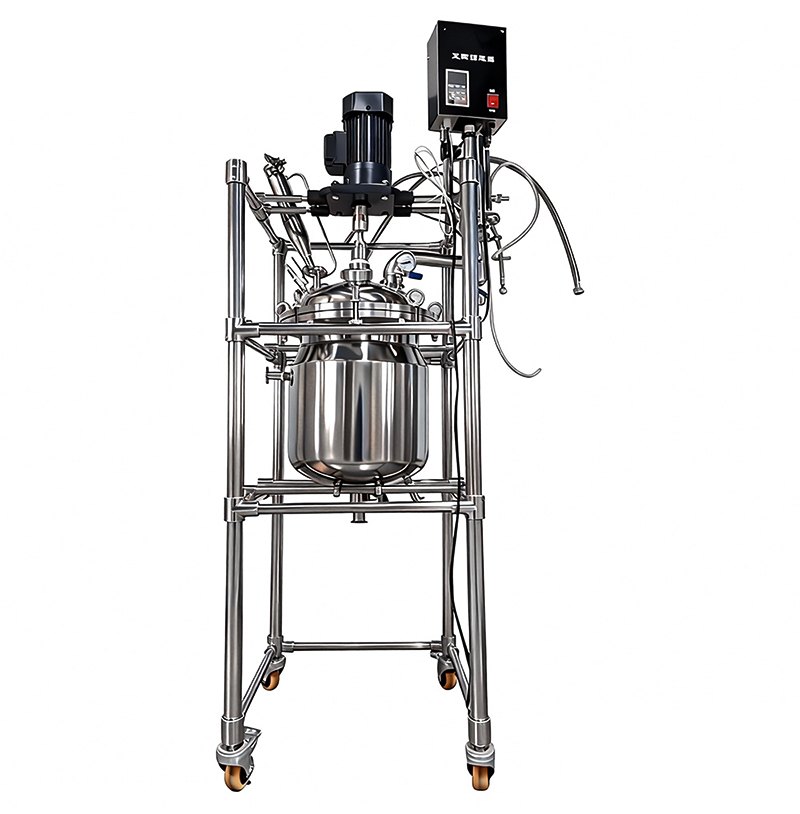
| One vessel for reaction and product recovery The AV-200R combines a 200 L jacketed reactor, agitator, large-area condenser, reflux line and 100 L receiver on one mobile frame. It supports batch reaction, mixing, vacuum distillation, solvent stripping and crystallization without transferring material between separate systems. SUS316L product-contact surfaces Double jacket for heating and cooling Mechanical seal with optional magnetic coupling Compact skid-mounted design | ||||
|---|---|---|---|---|
| 200 L | 100 L | 1.5 kW | 3 m² | |
| Reactor volume | Receiver volume | Agitator power | Heat exchange area | |
Product Advantages
- AV-200R is designed for pilot plants and small-batch production that require controlled reaction and efficient separation in a compact footprint.
- Main Configuration
- Standard configuration includes a jacketed reactor vessel, geared agitator, mechanical seal, large-area condenser, reflux piping, collection receiver, stainless support frame, valves and control cabinet. Magnetic coupling sealing and alternative voltages are available by request.
| AV-200R integrated reactor system | Integrated processing Run reaction, mixing, distillation, reflux and collection in one coordinated system. Improved vacuum stability Choose magnetic coupling sealing when the process requires stronger vacuum performance and lower seal leakage risk. Efficient thermal control The double-jacket vessel improves insulation, supports heating and cooling, and reduces hot-surface exposure. Higher condensation capacity A large-area condenser helps capture solvent vapor during distillation and residual-solvent removal. Flexible reflux operation Return condensate to the reactor for reflux or direct it to the receiver for solvent collection. Corrosion-resistant wetted parts SUS316L product-contact surfaces suit a broad range of laboratory and pilot-scale formulations. Practical installation The mobile stainless frame consolidates the vessel, drive, condenser and receiver for easier positioning and maintenance. |
Working Principle
Material enters the reactor through the KF25 feed port. The agitator maintains batch uniformity while thermal fluid circulates through the double jacket to heat or cool the vessel. Under vacuum, volatile components evaporate, pass through the condenser and collect in the 100 L receiver. Condensate can also return to the reactor through the reflux line.
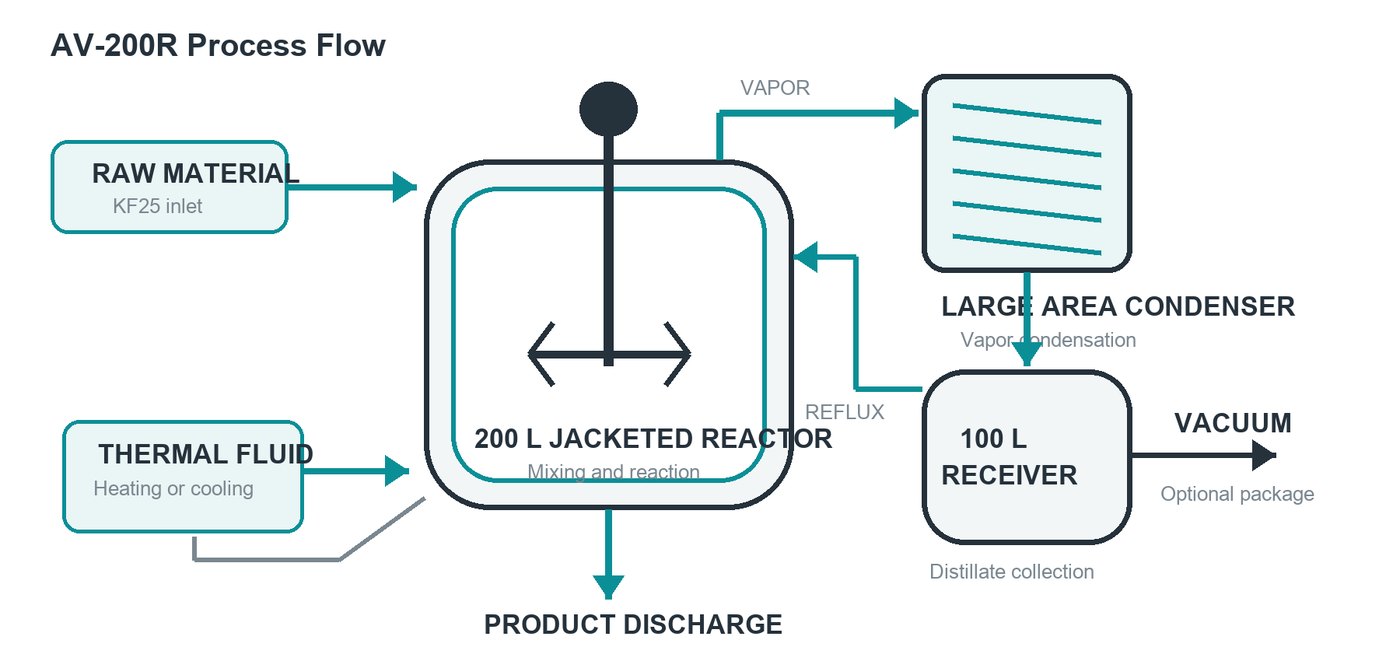
Simplified AV-200R process flow
| 01 Charge and condition Load the batch, start agitation and bring the jacket to the target process temperature. | 02 React or separate Run mixing or reaction. Apply vacuum for distillation, stripping or concentration when required. | 03 Condense and collect Condense vapor, select reflux or receiver collection, then discharge the finished batch. |
Technical Specifications
- The data below reflects the 200 L configuration. Final utility, seal and control selections should be confirmed in the quotation.
- Available Configuration Options
- Optional selections may include magnetic coupling sealing, process-specific agitation, alternative voltage and frequency, and matched vacuum or temperature-control equipment. Confirm chemical compatibility, operating temperature and vacuum requirements before ordering.
| Parameter | AV-200R Specification |
|---|---|
| Model | AV-200R |
| Reactor vessel volume | 200 L |
| Collection receiver volume | 100 L |
| Agitator motor power | 1.5 kW |
| Heat exchange area | 3 m² |
| Seal type | Mechanical seal; magnetic coupling seal optional |
| Feed inlet | KF25 |
| Jacket inlet and outlet | DN25 |
| Condenser coolant inlet and outlet | DN15 |
| Product-contact material | SUS316L |
| Other stainless components | SUS304, excluding fasteners |
| Power supply | 220 V, 50/60 Hz or 380 V, 50/60 Hz; other voltages optional |
| Overall dimensions | 235 × 105 × 257 cm (L × W × H) |
Applications
- The AV-200R is suitable for batch processes that combine agitation, controlled heating or cooling, and vapor recovery. The photographs below illustrate representative laboratory and pilot-plant environments.
| Natural Extract Decarboxylation Controlled thermal treatment of botanical and natural extracts. | Residual Solvent Removal Vacuum-assisted stripping after extraction or formulation. | Vacuum Distillation and Recovery Condensation and collection of reusable process solvent. |
|---|---|---|
| Chemical Reaction and Formulation Pilot-scale synthesis, dissolution and temperature-controlled reaction. | Mixing and Blending Uniform preparation of liquid and slurry batches. | Crystallization and Precipitation Controlled cooling, agitation and solids formation. |
Service & Contact
- Customisation — . Volume, agitator geometry, seal type and PLC package can be tailored to your recipe and target throughput.
- Warranty & support. 12-month limited warranty, lifetime remote technical support, on-site commissioning available.
- Lead time. Standard configuration ships in 15 working days; custom builds typically 25–30 working days.
More Reactors Overview
 AV20R
Lab Stainless Steel Reactor
The AV-20R is a 20-litre floor-standing reactor built around a SUS316L inner vessel, a vacuum-tight SUS304 jacket shell, a heavy-duty top-drive.
View Product →AV50RStainless Steel Multi-Function Reactor
The AV-50R is a 50-litre floor-standing reactor built around a SUS316L inner vessel, a vacuum-tight SUS304 jacket shell, a heavy-duty top-drive.
View Product →AV100RStainless Steel Reactor
Console view of the AV-100R — the left panel summarises the headline specs; the right side shows the jacketed vessel, reflux condenser and 1.5 kW top.
View Product →Reactors Overview
A jacketed reactor controls a reaction by controlling the temperature of the fluid circulating through the jacket that surrounds the vessel. Because heat is added or removed throug
Learn More →